
Specifying a Modbus Thermo-hygrometer to Survive High-Velocity Plenum Condensation
Why High-Velocity HVAC Plenums Destroy Standard Sensors
Duct sensor reliability is decided by the physical filter cap, not by the calibration certificate in the shipping box. Many HVAC procurement teams specify an expensive thermo-hygrometer probe only to watch its relative humidity reading flatline at 100% RH within its first winter. This field failure is rarely an electrical defect; it is a mechanical one. When duct airspeeds exceed 10 m/s, the kinetic force of the air strips water droplets directly off the cooling coils and blasts them down a 10 m duct section straight into the sensor. Instead of protecting the sensor, typical commercial probes with thin plastic slots trap this liquid moisture inside. This creates a localized, artificial 100% RH micro-environment that locks the sensor out long after the surrounding duct air has dried.
Once a probe hits saturation lockout, the system stops responding to actual conditions, turning your energy-saving economizer cycles into blind guesses. We often see field technicians try to patch this by applying software offsets in the building management system (BMS). It is a short-sighted fix that hides the real problem; subtracting a digital offset does nothing to stop a waterlogged sensing grid from corroding behind its plastic shield. At YGhao, we approach this by changing the physical boundary of the probe. Replacing a cheap slotted cap with a heavy-walled sintered metal or porous PTFE filter allows water vapor to diffuse naturally while blocking the high-velocity droplets that kill standard commercial sensors.
When specifying sensors for high-velocity plenums, remember that the physical robustness of the filter cap will dictate your long-term calibration stability far more than any precision rating printed on page one of the datasheet.
Filter Membranes and Transceiver Isolation: What Separates Industrial and Commercial Probes
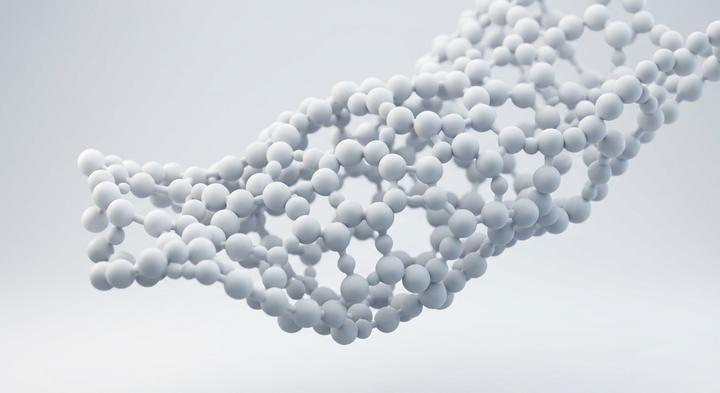
Figure 1: Conceptual rendering of a microscopic porous structure designed to block liquid carryover while allowing vapor to diffuse freely.
How do I choose a thermo-hygrometer probe that won’t fail when duct condensation occurs?
Selecting a high-performance thermo-hygrometer requires evaluating how its physical filter assembly and electrical transceiver handle aggressive condensation and electromagnetic noise. While commercial HVAC buyers often look only at basic accuracy percentages, industrial procurement officers must prioritize pore-size physical dynamics and galvanic line protection to avoid early field failures. These critical physical and electrical performance metrics define the operational boundaries of the instrument under real-world plenum stress.
| Sensor Grade (Buyer Class) | Filter Cap & Velocity Limits | Isolation & Noise Fit | Primary Failure Risks | Inquiry Verdict |
|---|---|---|---|---|
| Commercial-Grade (Light commercial contractors) | Slotted ABS or open nylon mesh; rated for velocities strictly below 5 m/s. Zero physical protection against water carryover. | None; shared power and signal ground with no isolation barrier. High vulnerability to common-mode voltage. | Sensor element flooding, structural cap shear, and chip washout. Complete lockouts lasting 12 to 24+ hours. | Avoid for supply plenums. Only specified for dry return air monitoring where budget overrides longevity. |
| Mid-Grade / OEM (Standard HVAC packages) | Porous PTFE hydrophobic membrane; rated for velocities up to 15 m/s. Repels light droplets but can choke vapor diffusion if coated. | Transient Voltage Suppressors (TVS) on RS-485 line. Modest static protection but vulnerable to persistent ground loops. | Membrane saturation, slow recovery times (15 to 45 minutes), and electrical noise disruption from adjacent machinery. | Acceptable for variable volume systems with moderate, non-condensing airflow and isolated wiring. |
| Industrial / Plenum-Grade (Heavy industrial / cleanrooms) | 20–50 Micron sintered stainless steel cap; rated for velocities exceeding 30 m/s. Robust, high-permeability physical shield. | Fully isolated RS-485 transceiver (up to 2.5 kV galvanic isolation) paired with dedicated TVS and optical isolation. | Minor debris accumulation over multi-year cycles. Sensor recovery from direct drenching takes less than 3 minutes. | Required for high-velocity plenums, humidifier zones, and high-noise VFD areas. Specify YGhao’s configured industrial line. |
Matching the Probe to Duct Dynamics: Standard Return vs. High-Velocity Supply Plenums
A pricing estimator looking at a 120-page schematic on a Monday morning usually spots the same lazy shortcut: a single, high-spec thermo-hygrometer part number copied and pasted across every zone from the basement mechanical room to the executive suites. Standardization looks great on a purchasing order, but it ignores the fundamental laws of Duct Dynamics. When you treat a low-velocity exhaust line the same as high-speed, humidified supply air, you are either throwing away thousands of dollars in margin or setting yourself up for a warranty callback when the sensors fail. Different zones present entirely distinct pressure and velocity profiles, meaning procurement needs to split the order based on actual operating conditions.
Commercial Office Return Ducts
In standard Commercial Office Return Ducts, air speeds stay low—usually under 5 m/s. The risk here isn’t physical shear or heavy condensation; it is the slow, silent buildup of ambient carpet fibers and drywall dust. For this type of Standard Return, paying for an exotic PTFE membrane is a waste of budget. A practical Low Air Velocity And low-stress environment requires only a cost-effective copper-sintered filter cap. This cap keeps the dust off the sensor element while allowing fast response times, and because there is no liquid water or aggressive electrical noise to worry about, a standard, non-isolated Modbus transmitter does the job perfectly without driving up unit costs.
Pharmaceutical Cleanroom Supply Plenums
Move over to Pharmaceutical Cleanroom Supply Plenums, and the operating environment changes completely. Air velocities jump to 12 to 15 m/s, carrying localized pockets of High Moisture from steam humidification cycles that can instantly saturate a standard commercial probe. A cheap sensor here will lock up or drift within weeks, dragging down the validation status of the entire cleanroom. For these Velocity Supply Plenums, you need a high-end industrial probe fitted with a hydrophobic PTFE membrane that repels liquid droplets while letting vapor diffuse. The electrical side is just as critical; because these plenums sit next to massive fan arrays and variable frequency drives, the transmitter must have isolated RS-485 transceivers to prevent ground loops from corrupting your data. Specifying a specialized, factory-configured remote probe from a manufacturer like YGhao protects the sensor elements from physical shearing while keeping your cleanroom validated.
Figure 2: Abstract airflow visualization highlighting high-velocity dynamics inside specialized supply plenums.
If you want to keep project costs down without risking field failures, remember this simple rule of thumb: buy cheap copper caps for your low-speed return paths, but never skimp on PTFE shields and isolated electronics for your high-velocity supply lines.
Three Spec-Sheet Traps That Lead to Early Field Failures
Physical operational conditions, not desktop datasheet numbers, dictate whether a duct sensor lives or dies in a real system. Most HVAC procurement teams treat a sensor spec sheet like a safe contract, assuming that if a thermo-hygrometer meets the nominal tolerances, it will survive its first winter. It rarely does. To prevent Early Field Failures Duct layouts require hardware built to handle physical abuse—kinetic water impact, chemical saturation, and electrical noise—that standard datasheets conveniently ignore.
“It says IP65 on the datasheet, so it’s fully protected against wet plenum environments.”
An IP65 rating is tested using static dust and gentle water splashes in a quiet lab. That rating is useless when air speeds cross 10 m/s inside an active supply duct. In those high-velocity conditions, micro-droplets turn into high-speed projectiles that punch right through standard rubber gaskets and drown the internal polymer. Instead of relying on a generic IP rating, you need a physical barrier—like a sintered stainless steel or porous PTFE filter cap—to diffuse that kinetic mist before it touches the active sensor element. YGhao configures these heavy filters specifically to slow down high-speed water droplets without lagging the response time.
“Both suppliers quoted ±2% RH accuracy, so the sensors will perform identically in our duct.”
On a clean calibration bench at 25°C, two different probes might align perfectly. But the moment condensation hits, they drift down completely different paths. A standard commercial-grade probe will lock out at 100% RH for hours or fail permanently as minerals from the duct water leach into its element, while a ruggedized sensor recovers its baseline within minutes of the air drying out. Don’t buy a dry-lab spec; ask your supplier for a post-saturation recovery curve to see how the sensor behaves after it gets soaked.
“As long as it supports Modbus RTU, we can daisy-chain it straight into our RS-485 loop.”
A cheap transceiver without galvanic isolation works fine on a desktop, but it can knock down your entire RS-485 loop when the big blower fans or VFDs kick in. Those heavy inductive loads dump massive voltage spikes back into your signal lines, corrupting Modbus data packets or outright frying the transceivers. If you want to protect the BMS network from dropping off-line, require at least 1.5 kV galvanic isolation and optical protection before signing off on a bulk order.
Are your current sensor specifications protecting your network from the physical realities of the duct, or are they just satisfying a paper checklist?
Vetting OEM Thermo-hygrometer Manufacturers for Quality and Compliance
How do I audit a thermo-hygrometer manufacturer’s calibration and sealing claims before signing off on a bulk order?
Look past the ISO 9001 frames on the wall. A framed certificate means the factory has a documented process for ordering stationery and checking badges; it does not mean their sensor batch will hold its calibration in a saturated supply duct. To get real verification, demand the raw, unedited environmental chamber logs from the specific production lot before it ships. Sourcing teams use a Technical Auditing Matrix to parse these documents, mapping each critical test to the specific engineer who must own the verification. This establishes the ‘Compliance How’ of your sourcing pipeline.
Technical Auditing Matrix
| Ask | Expected evidence | Red flag | Responsible party |
|---|---|---|---|
| Multi-point calibration verification | Original CNAS or NIST-traceable certificates showing testing at a minimum of 5 points across the 10% to 95% RH range at a constant 25°C, with raw deviation values logged. | Certificates showing only a single reference point (often 50% RH) or lacking a valid primary standard instrument identifier. | Quality Assurance Lead |
| Water ingress and seals testing | IP65 or IP67 test reports detailing continuous spray exposure targeting the seam between the probe tube casing and the internal wiring harness. | Epoxy potting used as the sole moisture barrier without secondary dual silicone O-rings or mechanical brass/stainless cable glands. | Lead Hardware Engineer |
| Custom firmware capabilities | Modbus RTU register mapping sheets showing configurable baud rates (e.g., 9600 to 115200 bps), parity adjustments, and non-volatile configuration memory. | Proprietary or hard-coded register maps that require external protocol translation gateways to talk to legacy Building Management Systems. | Systems Integration Lead |
| Under-pressure sensor drift | Certified logs showing sensor recovery and drift limits after a 48 hours high-velocity humidity cycle simulating duct saturation. | Drift listed as ‘typical’ on datasheets without defining the air velocity, temperature, or chemical exposure parameters of the test. | Quality Assurance Lead |
At YGhao, we run these tests in automated environmental chambers that query each thermo-hygrometer via Modbus during the cycle. Checking the sensor under real thermal and moisture stress is the only way to prove the internal wiring harness seal actually blocks micro-condensation bypass. Before releasing a production deposit, request a pre-calibrated sample set to your system’s exact register map and run it through your own test loop. If the supplier hesitates to write custom registers or provide raw calibration logs, they are running a high-volume assembly line, not an industrial OEM partnership.
Drafting the RFQ: Modbus Config, Probe Customization, and Sample Evaluation
Once you have matched your sensor to the actual duct dynamics and velocity profiles, those engineering decisions must be written into an RFQ that leaves zero room for factory assumptions. On the physical side, that means getting explicit about dimensions and materials: don’t write “standard length” when you need a 150mm or 200mm insertion depth in a heavy-walled 316L stainless steel probe to withstand turbulent supply air. Specify the exact adjustable duct-mounting flange and whether your environment requires heavy, corrosion-resistant stainless housings instead of cast aluminum. For Probe Customization, spell out the filter media—whether it is a porous PTFE membrane for rapid drying or a sintered metal shield to stop grit from eating the polymer element in dry, high-velocity plenums.
On the software side, the most expensive delays occur because a device ships with the wrong Modbus Config. To prevent your commissioning team from wasting days manually remapping registers on-site, your RFQ must dictate the exact baud rate (9600 or 19200 bps), parity (even, odd, or none), stop bits, and slave IDs before the shipment leaves the factory. We suggest coordinating a trial run; requesting a hardware trial is the best way to verify compatibility. Getting a physical trial unit allows for a hands-on Sample Evaluation While you finalize the physical and communication details. To simplify this setup, download YGhao’s standard Modbus register templates and engineering datasheets to map out your system, or contact our engineering team directly to request a custom-built test sample configured to your exact duct dimensions.




